5 Conveyor Design Choices That Make Belt Cleaners Easier to Maintain
Key Highlights
- Proper placement of primary and secondary belt cleaners depends on pulley sizes, belt path, and structural constraints to maximize cleaning efficiency.
- Choosing larger-diameter head pulleys and motorized drive pulleys can create more space for cleaners and improve fugitive material control.
- Designing platforms around belt cleaners reduces maintenance time and enhances safety, leading to lower operational costs.
- Accurate installation by trained professionals ensures optimal cleaner performance and minimizes belt damage risks.
- Using engineering calculations like DIN or CEMA methods helps in designing pulley wrap angles that facilitate cleaner mounting and maintenance.
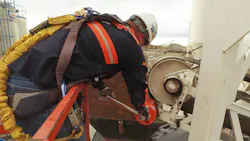
Getting belt cleaners into the right positions is a common hurdle to conveyor efficiency. Effective cleaning often runs up against structural design, tight spaces, and the need for safe access. This article covers where primary and secondary cleaners belong and the design choices that make room for them. [Figure 1]
Where CEMA Says Belt Cleaners Belong
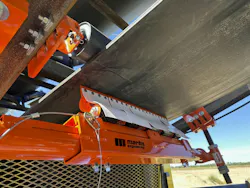
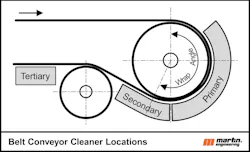
Primary cleaner placement is specified by the head pulley diameter and where the material leaves the belt. The Conveyor Equipment Manufacturers Association (CEMA) defines the secondary position as the space between the head pulley and the snub pulley on the return run of the belt. [Figure 2]
Unfortunately, structural designs often result in a very short section of belt surface between the head pulley and the snub pulley, which is the ideal location for many secondary cleaner designs. This limited distance leaves little room for belt cleaners in the secondary position.
Additionally, designers often place work platforms based on major components, overlooking access for belt cleaner inspection or maintenance. Belt cleaners typically require more attention than major components to ensure system efficiency because the blades are wear components that must be maintained at optimal cleaning pressures.
5 Design and Installation Tips
Five design choices can make room for more effective belt cleaning:
1. Question the Default Drive Pulley Wrap Angle
A common default wrap is 210 degrees, created by the position of the snub pulley. The gap between the head pulley and snub pulley is an ideal location for a secondary cleaner, but the combination of pulley diameters and wrap angle may make mounting a secondary cleaner difficult and maintenance nearly impossible. We recommend utilizing an updated engineering design program that uses either the DIN or CEMA methods for calculating accurate tension values. [Figure 3]
2. Choose a Larger-Diameter Head Pulley
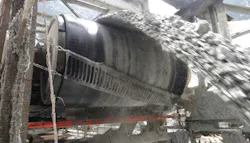
Choosing a head pulley based on the minimum diameter may seem like it saves money; however, the US Mining Safety and Health Administration (MSHA) reports that up to 85% of maintenance problems are due to fugitive materials, which increase costs for cleanup, labor, and equipment replacement. A larger head pulley can allow the installation of two cleaners in the primary position and enough snub pulley space for one or two cleaners in the secondary position, significantly reducing the amount of fugitive material.
3. Design Platforms Around Belt Cleaner Access
Maintenance personnel can spend up to a third of their time simply accessing equipment. Designing access to seldom-inspected or maintained components based on minimum walkway codes increases costs. Consider structures and work platforms that facilitate belt cleaner inspection and maintenance. [Figure 4]
4. Use Motorized Drive Pulleys to Free Up Space
Motorized pulleys offer energy advantages and weight savings and open up space for belt cleaner installation and maintenance. Since all rotating components (including the main bearings) are inside the pulley, the external stub shafts need minimal space to mount to the structure.
5. Rely on Trained Installers for Precise Mounting
Belt cleaners must be mounted accurately, typically within a few millimeters, to operate optimally and reduce the risk of belt damage. Partnering with the belt cleaner supplier ensures proper installation with minimal adjustments and helps the new chute maintain a clean, professional appearance.
The Bottom Line
A belt cleaner system should be properly specified, designed, and installed to gain the direct and indirect long-term cost benefits of reduced fugitive material, but compliance is also an issue. Safe access with adequate space for installation, maintenance, and inspection is critical to supporting longer system life and a lower cost of operation.
About the Author
R. Todd Swinderman
President, Emeritus | Martin Engineering
R. Todd Swinderman earned his B.S. from the University of Illinois, joining Martin Engineering's Conveyor Products division in 1979 and subsequently serving as V.P. and General Manager, President, CEO, and Chief Technology Officer.
Todd has authored dozens of articles and papers, presenting at conferences and customer facilities around the world and holding more than 140 active patents. He served as President of the Conveyor Equipment Manufacturers' Association (CEMA) and was the editor of CEMA's 6th and 7th editions of Belt Conveyors for Bulk Materials, The Design Guide for Belt Conveyors. Todd is active on several CEMA committees, including Chair of the Bulk Safety Committee, and is a member of the ASME B20 committee on conveyor safety, which sets U.S. conveyor safety standards.
Swinderman retired from Martin Engineering to establish his own engineering firm and currently serves the company as an independent consultant.