4 Factors to Weigh When Specifying Bulk Material Handling Systems
Key Highlights
- Material properties: particle size, shape, and hygroscopicity determine handling strategy and equipment selection from the start.
- Sealed containment: glove box interfaces and inert purging protect operators and product integrity when materials are oxygen-sensitive or hazardous.
- Enclosed conveyance: low-speed systems like tubular drag conveyors cut dust and contamination while preserving material integrity.
- Automation and compliance: PLC-driven dosing and clean-in-place design reduce manual error and maintain consistency over time.
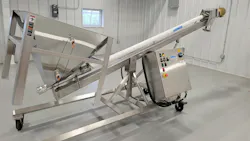
Containment, conveyance, automation, and compliance all stem from one starting question: what will the material do?
Powder and granule handling in chemical manufacturing has always required precision, but today's production environments elevate that requirement. Materials vary widely in bulk density, flow properties, reactivity, and contamination risk. Many behave unpredictably when exposed to humidity or oxygen, while others present combustible dust hazards that demand verified protection. Designing a system that moves these materials reliably is no longer just a mechanical problem but a multivariable engineering challenge shaped by material science, process control, and environmental safety.
What defines smart bulk material handling today is not the presence of new equipment types but the ability to engineer material-appropriate, sealed, and automated systems that protect operators, maintain product integrity, and ensure consistent throughput. Achieving this requires a deeper understanding of how powders behave, how conveying environments influence that behavior, and how containment and control must adapt to the material, not the other way around.
Start With Material Behavior
Engineering a bulk material handling system for chemical processing begins with a single question: what is the material going to do once it enters the equipment? Particle size and shape, cohesiveness, hygroscopicity, and bulk density directly influence whether a material will move freely, form agglomerations, degrade under mechanical stress, or absorb moisture during conveying. Even the packaging format, such as kraft bags, drums, totes, or bulk bags, affects how predictably material feeds into the system.
Flow mode also matters. Batch operations require tight control on dosing and isolation, while volumetric or continuous processes need steady-state movement that prevents starvation or surging. Intermittent flow behaves differently than uninterrupted flow, and each scenario places unique demands on receiving equipment, conditioning stages, and conveyor selection.
Designing with these material properties in mind helps ensure stability across the line. Materials that generate dust clouds during emptying require sealed transitions rather than open discharges. Powders that form hard agglomerates may require conditioning before conveying. Oxygen-reactive compounds need inert gas environments to prevent oxidation or decomposition. These considerations are technical, but they are foundational. Without them, even well-built equipment will underperform.
Gaining this level of insight almost always starts with detailed, upfront conversations with plant teams about material characteristics, packaging, flow modes, and process constraints.
Containment and Atmospheric Control
The point where operators interact with raw material is also the point where risk is highest. This is why modern chemical plants increasingly rely on glove box interfaces that create a sealed environment for opening and emptying raw material packages. These systems are not simply barriers; they are engineered environments with defined atmospheric conditions.
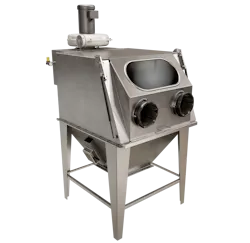
When a hazardous or oxygen-sensitive material is loaded into the glove box, the chamber is sealed and purged, often with nitrogen, until oxygen levels drop to a safe threshold. Only then does the operator receive a visual signal indicating that it is safe to open the package. Once emptied, the material moves into a closed conveying path, and the chamber is returned to the ambient atmosphere so the operator can remove the empty packaging. This cycle establishes a predictable, repeatable method for isolating materials from both operators and the external environment.
For materials that react with oxygen, the purge process is essential to prevent unwanted chemical reactions. For materials that are hazardous to people, containment eliminates dust exposure and airborne particulates. In both cases, predictable atmospheric conditions protect product integrity and minimize cross-contamination risks.
Environmental classification further shapes design. In facilities where combustible dusts or volatile compounds are present, explosion-proof controls and classified area-rated components become mandatory. Matching controls and components to the correct area classification is fundamental to protecting operators, preventing ignition of combustible dusts, and maintaining compliance with plant and regulatory safety requirements over the life of the system. Engineering compliance requires more than simply meeting code; it requires designing systems that will continue to behave safely over time as materials, conditions, and processing steps evolve.
Sealed Conveyance and Mechanical Design
Once material leaves the unloading zone, the method of conveyance has a direct impact on its quality and the cleanliness of the plant environment. In many chemical facilities, bulk bags are still discharged directly into open vessels, a method that moves large quantities quickly but releases dust, causes material loss, and introduces safety hazards. Shifting bag handling to floor-level, fully enclosed discharge points improves plant air quality by containing airborne dust, vapor, and odor, while also reducing operator exposure and the likelihood of flammable dust or vapor ignition. Enclosing the conveyance path eliminates these concerns and creates a more controlled environment for sensitive materials.
What Hapman Brings to These Scenarios
Hapman, a global manufacturer of bulk material handling systems, designs equipment for chemical, pharmaceutical, food, and specialty material industries, with systems built around dust-tight, sealed conveyance; inert purging capability; washdown-ready configurations; and flexible control integration. The company's engineering approach centers on adapting system architecture to a facility's specific material properties, safety demands, and operational constraints rather than applying a standard design across applications.
Tubular drag conveyors are frequently selected for their ability to move powder gently and consistently. They operate at low speeds and move material en masse rather than accelerating individual particles, often below 40 feet/min (12 meters/min). This combination of slow velocity and high torque reduces particle degradation, preserves blend uniformity, and minimizes segregation. Because the system is sealed, powders remain isolated from humidity or oxygen, and the line itself can be purged with nitrogen when inert conditions are required.
Mechanical considerations play a significant role in performance. Lower speeds decrease frictional heat, lowering the risk of ignition when handling combustible dust. Higher torque enables the conveyor to move material with less horsepower, improving energy efficiency. Throughput is dictated by conveyor diameter, which can range from 3 to 12 inches (7.6 to 30.5 cm) depending on the volume and physical properties of the material. These engineering details are not incidental. They define operational stability and long-term reliability.
Automation and Compliance
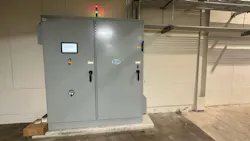
Automation has become a central component of chemical processing, especially where manual weighments or bag counting introduce variability or ergonomic strain. Automated batching, recipe control, and PLC-driven sequencing offer consistent dosing and batch integrity. Modern systems integrate easily into plant controls through hardwired connections or Ethernet links, reducing commissioning time and improving interoperability across legacy and new equipment.
High-purity or contamination-sensitive processes require even greater control. Dust-tight construction prevents particulate migration, while inert gas purging safeguards reactive powders. Surface finishes matter. Polished internal and external surfaces simplify wipe-down cleaning while Clean-in-Place configurations support validated washdown processes. Material compatibility, from stainless steel to specialized plastics and elastomers, ensures equipment durability when handling corrosive or chemically aggressive powders. The ability to specify different steels, plastics, and elastomers to coexist with diverse chemical profiles is often what allows a system to meet both performance and compliance requirements in a given facility.
The Bottom Line
Smarter bulk material handling in chemical manufacturing ultimately hinges on accurately anticipating how powders behave and designing systems that account for those behaviors at every stage. Particle dynamics inform equipment selection. Environmental conditions, including oxygen exposure, humidity levels, and classified-area requirements, influence containment strategies. Mechanical design choices establish whether material moves gently, predictably, and without degradation. Control interfaces, automation architecture, and materials of construction determine whether the system remains stable, hygienic, and compliant over time.
The equipment should reflect the realities of the material and the process, not the reverse. For engineers and plant managers evaluating a new system, that means starting every specification conversation with the material itself—its behavior, hazards, and packaging—before a single piece of equipment is chosen.